Selecting the right Kraft Paper Tape Laminating Machine is a production decision, not a catalogue exercise. Packaging lines now face stronger pressure to reduce plastic use, improve recyclability, and control operating costs. Smithers’ report, The Future of Global Packaging to 2028, identifies sustainability and material efficiency as major forces shaping packaging investment. These trends make kraft paper tape increasingly relevant for carton sealing, bundling, and industrial packaging applications.
However, a greener material does not guarantee efficient production. A suitable machine must match paper grammage, tape width, adhesive chemistry, coating weight, drying capacity, and expected line speed. Small differences matter. Excessive web tension can wrinkle a 60-gram kraft paper roll. Poor adhesive control can create edge lift after storage. A slow drying section may reduce output during humid weather. These details deserve practical testing.
Performance matters most.
PMMI industry reports consistently emphasize automation, uptime, labor efficiency, and flexible equipment design as key packaging machinery priorities. Therefore, buyers should examine measurable evidence, including stable tension control, coating uniformity, changeover time, energy consumption, and reject rates. Factory trials are valuable because laboratory samples rarely reveal every production problem. I have seen specifications look convincing until operators tested actual paper rolls and adhesive batches.
This guide explains how to evaluate a Kraft Paper Tape Laminating Machine with technical judgment. It also questions common assumptions, including the belief that maximum speed always delivers the best return. A reliable machine should support consistent quality, maintainable operation, and realistic growth. The final choice should reflect current production needs, operator experience, and verified supplier performance.
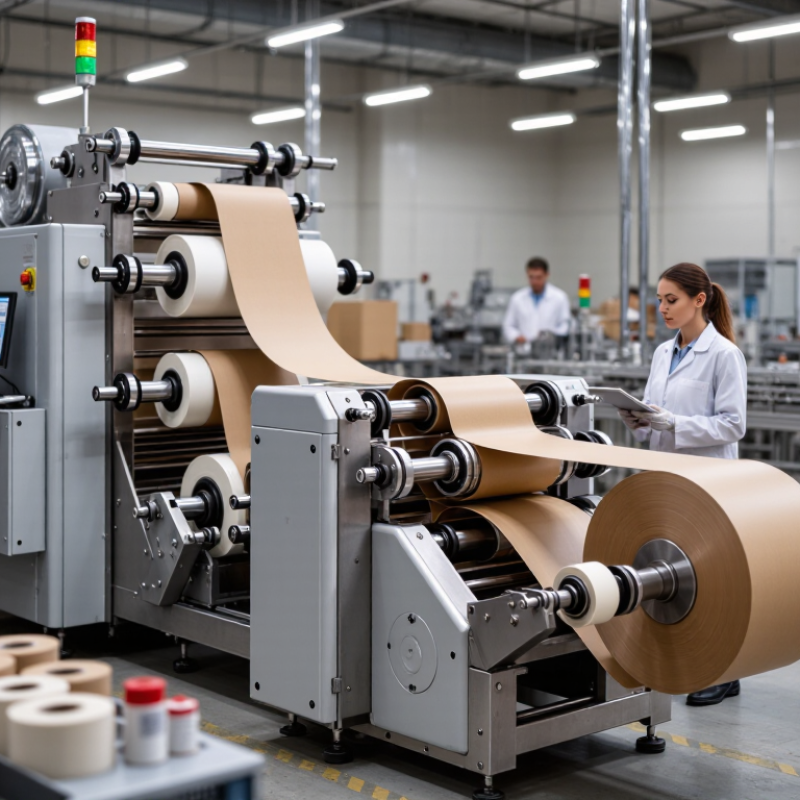
A kraft paper tape laminating machine bonds paper with adhesive, film, or another functional layer. Its core work involves unwinding, coating, laminating, drying, and rewinding. Each stage affects tape strength and appearance. A stable tension system prevents wrinkles along the roll. Heated rollers may improve bonding, but excessive heat can weaken paper fibers. Ask about substrate width, thickness, adhesive type, and production speed before choosing equipment. These details determine whether the machine suits your actual process.
Tips: Request a trial using your kraft paper, adhesive, and target width. Inspect the sample under bright light. Look for bubbles, edge lifting, uneven coating, and loose winding. Check whether operators can adjust pressure and tension without complicated procedures. A clear control panel also reduces training time. Do not judge performance from speed alone.
In practical testing, a machine may perform well at low speed but struggle during continuous production. That difference matters. Review drying capacity, roller alignment, cleaning access, and spare-part availability. Ask how often key parts require inspection. Reliable machines usually provide measurable settings and repeatable results. However, no selection is perfect. Paper humidity, adhesive viscosity, and operator habits can still change the outcome. Keep test records, including room conditions and batch details. This helps identify whether a defect comes from the machine or the material.
Begin with the tape structure, not the machine brochure. Kraft paper may be coated, uncoated, creped, or reinforced with fibers. Each surface reacts differently to pressure, heat, and adhesive moisture. Record the paper thickness, roll width, adhesive type, and liner weight. Small differences matter.
Check whether the adhesive needs drying, heating, or simple pressure bonding. Water-based adhesives often require controlled drying zones and steady airflow. Hot-melt adhesives demand accurate temperature control. Solvent-free systems may simplify operation, but they still need suitable web tension. Ask for material samples before selecting equipment. A clean test roll reveals more than a sales claim.
Production targets shape the machine specification. Measure the required speed, daily output, splice frequency, and finished roll diameter. A narrow trial line cannot represent a high-volume process. Confirm the usable width and minimum slitting size. Also inspect tension controls, edge guidance, roller hardness, and cleaning access. These details affect wrinkles, telescoping, and uneven lamination.
In practical trials, the first result is rarely perfect. That is normal. Test several tension settings and compare peel strength, flatness, and winding quality after conditioning. Keep written records, including room temperature and humidity. I have found that operators often notice problems before instruments do. Their observations deserve a place in the specification. Leave room for adjustment, because paper behavior changes between batches.
Choosing a kraft paper tape laminating machine starts with production volume, tape width, and adhesive requirements.
Semi-automatic models suit small batches and frequent product changes. Operators load rolls manually and adjust tension by hand. They cost less, but output can vary between shifts.
Fully automatic lines support continuous unwinding, laminating, slitting, and rewinding. They reduce handling time but require better training and maintenance.
Check the specifications closely.
Useful working widths usually range from 300 to 1,600 millimeters. Line speed may range from 20 to 150 meters per minute. Higher speed is not always better.
The laminating roller should provide stable pressure across the entire web. A tension controller helps prevent wrinkles, edge curling, and uneven winding.
For water-based adhesives, drying capacity and airflow deserve special attention. Hot-melt systems need accurate temperature control and insulated adhesive paths.
Ask about coating accuracy, shaft size, maximum roll diameter, and power consumption.
A practical setup may include automatic edge alignment, a touch-screen control panel, and emergency stop protection. These features improve daily operation, but they also add complexity.
During testing, inspect the tape after several hours, not only after startup. I have seen clean first rolls become loose later.
That usually indicates poor tension control or incorrect adhesive curing.
Request sample trials using your actual kraft paper, liner, and adhesive before approving the machine.
How to Choose a Kraft Paper Tape Laminating Machine?
Choosing a kraft paper tape laminating machine starts with your real production rhythm, not the maximum speed in a brochure. Measure rolls per shift, web width, coating thickness, and planned downtime. A machine rated for 80 meters per minute may run closer to 55 when adhesive viscosity changes. That gap matters. Leave room for seasonal orders, but avoid buying capacity that sits idle.
Quality control should be visible at the operator’s station. Look for stable tension control, accurate temperature settings, edge alignment, and easy access to inspection points. Test samples should show even bonding, clean edges, and no wrinkles after storage. Ask how calibration records are maintained and how faults are logged. In my experience, small alarms prevent large waste, although operators sometimes silence them too quickly. Energy use also deserves measurement. Compare heater efficiency, motor load, standby consumption, and heat recovery options. Request data from a normal shift, not laboratory conditions. A lower-power machine can still cost more if it causes rework or long warm-up periods.
Tips: Run a timed trial with your own kraft paper and adhesive. Record output, rejected rolls, kilowatt-hours, and changeover time. Check noise and heat around the machine. Do not trust one perfect sample. Repeat the test after adjustments, because real production is rarely so cooperative.
A reliable supplier should understand your kraft paper, adhesive, roll width, and production speed. Ask for test runs using your actual materials. Samples can reveal wrinkles, weak bonding, and uneven edges before purchase. Request clear records for tension settings, roller pressure, curing conditions, and output inspection. Experienced suppliers should provide installation support, operator training, safety guidance, and practical maintenance documents. Speak with existing users if possible. Their comments often reveal response times that brochures do not mention.
Machine maintenance begins with a written routine, not a last-minute repair. Operators should inspect rollers, bearings, belts, sensors, and unwind brakes each shift. Remove adhesive residue before it hardens. Even a thin layer can change web alignment. Check electrical cabinets for dust and loose connections during planned shutdowns. Keep critical spare parts available, especially cutting blades, heating elements, seals, and tension-control components. Record each adjustment, fault, and replaced part. These notes help technicians identify repeated problems instead of guessing.
In daily production, cleaning may be delayed when orders become urgent. I have made that mistake. The result was uneven lamination and extra material waste. A realistic plan should include short cleaning windows, monthly inspections, and a yearly review with the supplier. Maintenance intervals may need adjustment after observing actual wear. Do not treat the manual as perfect. Your paper dust, adhesive formula, and working climate may require different decisions.
This site uses cookies. By continuing to browse the site, you are agreeing to our use of cookies.
OKLearn moreWe may request cookies to be set on your device. We use cookies to let us know when you visit our websites, how you interact with us, to enrich your user experience, and to customize your relationship with our website.
Click on the different category headings to find out more. You can also change some of your preferences. Note that blocking some types of cookies may impact your experience on our websites and the services we are able to offer.
These cookies are strictly necessary to provide you with services available through our website and to use some of its features.
Because these cookies are strictly necessary to deliver the website, refusing them will have impact how our site functions. You always can block or delete cookies by changing your browser settings and force blocking all cookies on this website. But this will always prompt you to accept/refuse cookies when revisiting our site.
We fully respect if you want to refuse cookies but to avoid asking you again and again kindly allow us to store a cookie for that. You are free to opt out any time or opt in for other cookies to get a better experience. If you refuse cookies we will remove all set cookies in our domain.
We provide you with a list of stored cookies on your computer in our domain so you can check what we stored. Due to security reasons we are not able to show or modify cookies from other domains. You can check these in your browser security settings.
We also use different external services like Google Webfonts, Google Maps, and external Video providers. Since these providers may collect personal data like your IP address we allow you to block them here. Please be aware that this might heavily reduce the functionality and appearance of our site. Changes will take effect once you reload the page.
Google Webfont Settings:
Google Map Settings:
Google reCaptcha Settings:
Vimeo and Youtube video embeds:
