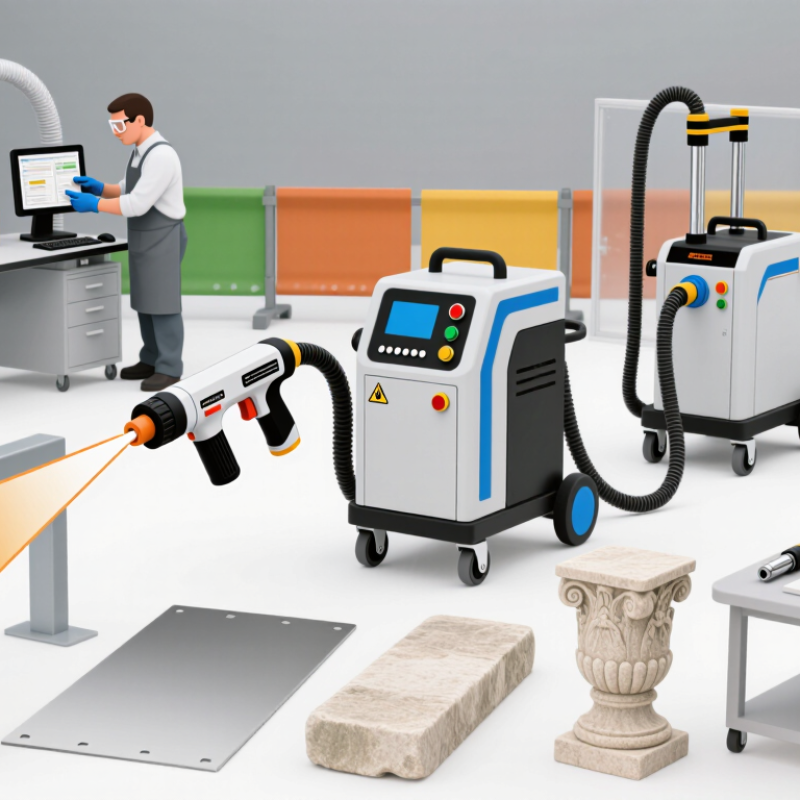
Choosing the right Laser Cleaning Equipment starts with the surface, not the machine’s headline power rating. A steel bracket with light rust needs a different approach from a painted aluminum panel or a delicate stone feature. The wrong settings can discolor, pit, or otherwise damage a workpiece. Small test areas matter.
Before comparing models, define the contaminant and the required finish. Is the target rust, paint, oil, oxide, or residue inside a narrow seam? Note the part’s material, size, shape, and condition. Then compare laser type, average power, pulse energy, repetition rate, scan width, and working distance against the actual task. Specifications only make sense in context. A higher power rating is not automatically better.
Also consider the conditions around the job. Check whether the equipment supports suitable fume extraction, protective enclosures, safety interlocks, and clear operating guidance. Ask suppliers about sample testing, maintenance intervals, replacement parts, training, and response times for service. A live demonstration on representative material can reveal details that a brochure cannot. Watch for uneven cleaning, heat marks, slow coverage, and awkward access around edges. That takes testing.
There is no universal setting or perfect machine for every workshop. Results depend on the material, contamination, operator technique, and process conditions. Even experienced teams may need to adjust their assumptions after a trial. This guide explains how to compare equipment practically, ask more useful supplier questions, and select a system that fits the work without overlooking safety, upkeep, or the limits of laser cleaning.
How to Choose the Best Laser Cleaning Equipment?
Laser cleaning removes rust, paint, oil, or oxide by directing concentrated light at a surface. The contaminant absorbs energy and heats rapidly; depending on the settings, it may vaporize or break away. The base material responds differently according to its alloy, coating, and condition. That variation matters. Laser cleaning is not simply “point and clean.” Pulse duration, power, scan speed, and working distance all affect the result.
The process is used to prepare metal parts before welding, clean tools and molds, and remove corrosion from equipment. It can also help clean delicate surfaces, but that does not mean every material is suitable. In practice, an initial pass may look uneven, and hidden coatings or surface damage can complicate the job. Check the substrate and test a small area before choosing equipment. A clean appearance alone does not confirm that the surface is undamaged.
Tips: Match the laser’s power and pulse settings to the material and contaminant. Use suitable eye protection and fume extraction, especially when coatings are present. Record test settings; small changes can affect cleaning quality.
Common laser wavelengths used in cleaning systems
Laser cleaning removes contaminants by directing controlled laser energy at a surface. Near-infrared 1064 nm systems are widely used in industrial cleaning; 532 nm and 355 nm options are also available for applications that benefit from different absorption characteristics. Wavelength alone does not determine the best equipment: match the laser to the substrate, contaminant, required throughput, and surface-finish limits, and validate the settings on a sample.
Choosing laser cleaning equipment starts with identifying what must be removed. Rust, paint, oil, and oxide scale respond differently to laser energy. Note the contaminant’s thickness, coverage, and bond to the surface. A thin oxide layer on steel is not the same job as several paint layers on a delicate component.
Then assess the base material and the desired finish. Steel, aluminum, stone, and composite surfaces tolerate different amounts of heat and energy. Decide whether you need complete removal, light surface preparation, or selective cleaning that preserves an underlying coating. Define practical limits too, such as acceptable discoloration, surface texture, and cleaning speed. Test a small, inconspicuous area before setting production parameters. Results can vary more than expected.
Tips: Ask for trials using your actual contaminant and material, not a similar sample. Check whether the system allows controlled adjustments to pulse energy, spot size, and scan speed. Provide suitable ventilation and dust collection for released particles. Keep records of settings and results; one overlooked variable can change the finish.
Laser cleaning equipment should be compared by laser type, power, and operating mode—not by wattage alone. Pulsed lasers deliver energy in short bursts, which can remove rust or paint while limiting heat buildup on thin metal. Continuous-wave systems provide a steady beam and can clean robust surfaces faster, but may leave more heat in the workpiece. Fiber lasers are common for metal cleaning; the best choice still depends on the material and contamination.
Power is not everything. Check pulse energy, repetition rate, spot size, and scanning speed together. A high-power unit can damage a delicate surface if its settings are poorly matched. Test a sample first. A small, marked test area can reveal discoloration or surface changes before full production. I would not claim one setting suits every job; it rarely does.
Tips: Match protective eyewear to the laser wavelength, and use suitable fume extraction. Compare handheld and automated modes, too: handheld units offer flexibility for awkward parts, while automated systems can give more consistent coverage. Ask for a practical demonstration on a sample similar to your workpiece. Record the settings and inspect the surface under bright, angled light; missed patches can be easy to overlook.
Assess Safety Features, Portability, and Maintenance Needs
When comparing laser cleaning equipment, examine its safety controls before focusing on output. Check for beam shields, emergency stops, interlocks, and clear warning indicators. The manual should specify eye protection for the equipment’s wavelength and operating conditions. Never assume ordinary safety glasses are sufficient. Reflective surfaces, nearby workers, and poor ventilation can all affect a work area’s risk. A tidy demonstration may not reveal these challenges.
Portability matters when equipment moves between a workshop, a vehicle frame, and tight corners. Compare the complete system’s weight, including the cleaning head, cables, and extraction unit. Check whether handles feel comfortable and cables catch on nearby fixtures. A compact unit may be easier to carry, yet a short hose or awkward control can slow the job. Try a realistic setup if possible. Small details matter.
Maintenance should fit your staff and schedule. Ask how often filters, lenses, and cooling components need inspection. Look for accessible service points and clear fault indicators. Dust around vents is easy to miss, and it can shorten component life. Keep essential consumables available, but make sure staff know how to identify and store them. No system is maintenance-free. Record cleaning intervals during use, then reconsider them when working conditions change.
Choose laser cleaning equipment by testing it against the actual task, not its advertised maximum power. Prepare coupons from the same material and contamination found on site. Test a small range of pulse energy and scan speeds. Record cleaning time, surface temperature, visible residue, and any change in surface texture. For steel that will be coated, compare results with ISO 8501-1 cleanliness grades, including Sa 2½, and assess remaining dust using the ISO 8502-3 tape method. These checks make comparisons more repeatable. A clean-looking panel can still hide residue.
Tips: Test edges, seams, and flat areas. Keep the nozzle distance and angle consistent. Photograph each coupon under the same lighting.
The NACE IMPACT study estimated global corrosion costs at US$2.5 trillion in 2013, or about 3.4% of global GDP. It also estimated that corrosion-control practices could save 15–35% of those costs. This is not a laser-cleaning performance benchmark, but it shows why preserving the substrate matters. Compare each system’s cleaning rate with its effect on the surface, then repeat the test on more than one coupon. Results may vary with coating thickness, rust scale, and operator technique. Record those limits instead of treating one successful pass as proof.
| Equipment Type | Typical Laser Output | Best-Suited Cleaning Requirements | Typical Contaminants | Cleaning Speed Potential | Substrate Control | Key Performance Test |
|---|---|---|---|---|---|---|
| Pulsed fiber laser cleaner | Typically 20–500 W average power; short pulses, often in the nanosecond range | Precision work, localized cleaning, thin coatings, and applications where heat input must be controlled | Oxide films, light rust, paint, and surface residues | Low to moderate; depends on pulse energy, scan width, and number of passes | Generally offers good control on suitable metals, but settings must be tested to avoid surface marking or damage | Compare removal rate and surface condition at several power, frequency, and scan-speed settings |
| Continuous-wave fiber laser cleaner | Commonly about 500–3,000 W; continuous output | Large-area cleaning and higher-throughput removal on robust metal surfaces | Heavy rust, thick oxide, and some paint or coating layers | Moderate to high on compatible surfaces; actual throughput varies with contaminant thickness | Higher heat input can increase the risk of discoloration, warping, or surface alteration on thin or heat-sensitive parts | Measure area cleaned per minute while checking surface temperature, roughness, and dimensional change |
| High-power continuous-wave system | Often above 3,000 W, depending on the system configuration | Large, heavily contaminated workpieces where production throughput is a priority | Thick rust, scale, and tenacious surface deposits on suitable materials | High potential on large areas, subject to safe operating distance and process validation | Requires careful control because concentrated heat can affect the base material | Run a production-scale trial and inspect for residual contamination, heat effects, and repeatability |
| Compact handheld laser cleaner | Usually a lower-power configuration; available as pulsed or continuous-wave equipment | On-site maintenance, small parts, weld areas, and locations that are difficult to move to a fixed station | Light to moderate rust, oxide, paint, and localized residues | Low to moderate; operator movement and access strongly affect results | Depends on laser mode and operator technique; use a test area before cleaning valuable surfaces | Check cleaning consistency across operators, reach, setup time, and results on representative parts |
| Automated or integrated laser cleaning cell | Power and pulse mode selected to match the part and production process | Repeated, high-volume jobs requiring consistent coverage and integration with a production line | Process-specific rust, oxide, coatings, or residues | Potentially high and repeatable after process optimization | Can provide consistent control when part positioning, fixturing, and laser parameters are validated | Verify cycle time, coverage, part-to-part consistency, and safety interlocks during a sustained production trial |
| Requirement to verify | Confirm average power, pulse energy (if applicable), pulse duration, repetition rate, and wavelength from the equipment specification | Define the target material, contaminant, required cleanliness, acceptable surface finish, and production rate before selection | Test the actual contaminant and its thickness; mixed or layered deposits may need different settings | Record cleaned area per minute or cycle time using a representative part and a consistent measurement method | Inspect for discoloration, roughness change, pitting, warping, and any effect on coatings or underlying material | Request a sample trial using the intended material and contamination level; compare results against written acceptance criteria |
| Note: Power ranges and performance descriptions are general examples, not guaranteed specifications. Actual results depend on laser parameters, optics, scan pattern, working distance, material, contaminant, and operating conditions. Follow the equipment safety instructions and applicable laser-safety requirements. | ||||||
This site uses cookies. By continuing to browse the site, you are agreeing to our use of cookies.
OKLearn moreWe may request cookies to be set on your device. We use cookies to let us know when you visit our websites, how you interact with us, to enrich your user experience, and to customize your relationship with our website.
Click on the different category headings to find out more. You can also change some of your preferences. Note that blocking some types of cookies may impact your experience on our websites and the services we are able to offer.
These cookies are strictly necessary to provide you with services available through our website and to use some of its features.
Because these cookies are strictly necessary to deliver the website, refusing them will have impact how our site functions. You always can block or delete cookies by changing your browser settings and force blocking all cookies on this website. But this will always prompt you to accept/refuse cookies when revisiting our site.
We fully respect if you want to refuse cookies but to avoid asking you again and again kindly allow us to store a cookie for that. You are free to opt out any time or opt in for other cookies to get a better experience. If you refuse cookies we will remove all set cookies in our domain.
We provide you with a list of stored cookies on your computer in our domain so you can check what we stored. Due to security reasons we are not able to show or modify cookies from other domains. You can check these in your browser security settings.
We also use different external services like Google Webfonts, Google Maps, and external Video providers. Since these providers may collect personal data like your IP address we allow you to block them here. Please be aware that this might heavily reduce the functionality and appearance of our site. Changes will take effect once you reload the page.
Google Webfont Settings:
Google Map Settings:
Google reCaptcha Settings:
Vimeo and Youtube video embeds:
