Choosing the right coating machine parts is not a simple matter of matching a part number. The right choice depends on the coating material, operating temperature, line speed, and finish your process needs. A doctor blade that works well with a thin liquid coating may wear quickly with a more abrasive formula. A roller with the wrong surface can leave visible streaks across a sheet. Small mismatches matter.
Before comparing suppliers, inspect the machine and record its model, part dimensions, material, and working conditions. Check how the component contacts the coating. Does it face heat, pressure, or repeated cleaning? These details help narrow the options and reduce avoidable downtime. A polished photograph is not enough. Ask for a drawing, material specification, and compatibility information.
The requested expert quotation cannot be verified from the supplied material, so I won’t attribute invented words to a named specialist. A practical rule for this guide is: “Choose a part for the process it must handle, not just the machine it must fit.” Treat that as editorial guidance, not a sourced quotation. Even careful selection has limits; installation, maintenance, and operating habits also affect performance. Sometimes the best part is not the most expensive one. It is the one whose specifications match the real conditions on your production line.
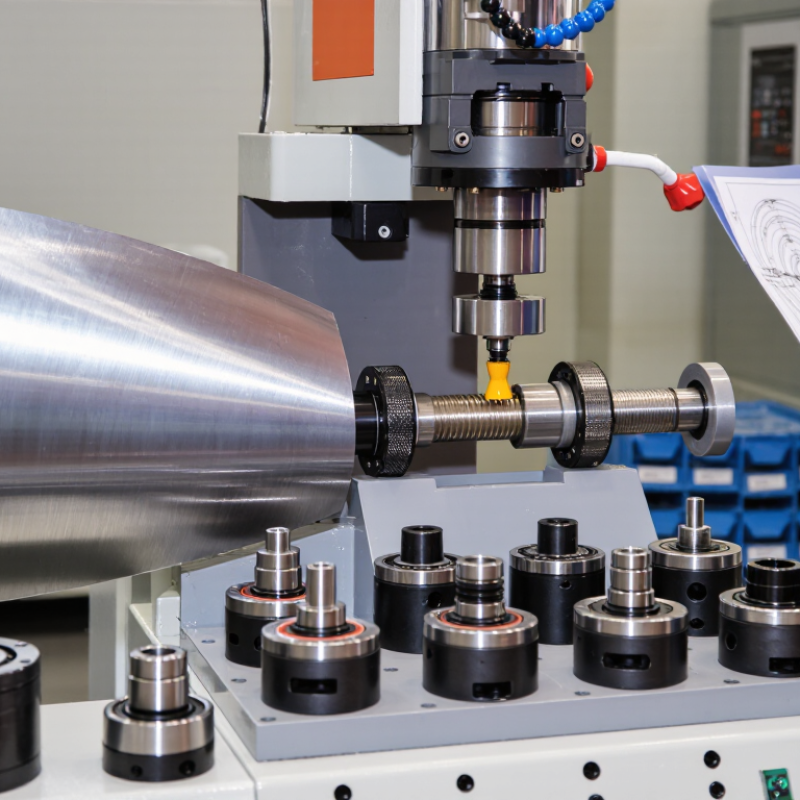
Before ordering parts, identify how the machine moves, applies, and cures the coating. A roll-to-roll line feeds a continuous web across rollers; a spray system atomizes liquid through a nozzle; a dip line immerses parts in a tank. Each creates different wear points. Rollers need the correct surface and alignment, while spray systems depend on clean fluid passages and compatible seals. A small mismatch can cause streaks, uneven film thickness, or repeated stoppages.
Then map the operating sequence: material feed, surface preparation, coating, drying or curing, and discharge. Note the coating’s viscosity, temperature, line speed, and cleaning method. These details help distinguish a pump seal exposed to solvents from a bearing near a hot curing zone.
The World Paint & Coatings Industry Association’s 2022 industry report estimated global coatings sales at about 56 billion liters. That scale reflects many formulations and processes, not one universal machine setup. The figure is useful context, but it cannot specify a replacement part.
Check the machine manual and compare the failed component with its operating conditions. A spray nozzle may look intact yet produce an uneven fan after partial blockage. It happens. Also record when the fault appears: startup, steady operation, or cleaning. This evidence narrows the likely cause, though it will not always identify it on the first inspection.
Define each coating machine part by the work it must perform, not just its material or price. A spray nozzle needs a stable flow rate and a wear-resistant orifice; a metering roller needs consistent surface finish and runout. Record the coating’s viscosity, temperature, solvent exposure, and any abrasive pigments. Then specify measurable limits, such as flow variation, operating temperature, dimensional tolerance, and acceptable downtime. Small details matter. A tiny change in nozzle wear can alter the spray pattern, while a seal that swells may cause leaks. These requirements should come from process trials and maintenance records, not assumptions alone.
Tips: Build a one-page part specification. Include the operating range, inspection method, replacement interval, and failure symptoms. Check the part under real production conditions; a laboratory result may not tell the whole story.
Durability deserves careful attention where parts contact corrosive coatings or cleaning fluids. NACE International’s 2016 IMPACT study estimated global corrosion costs at US$2.5 trillion annually, or 3.4% of global GDP. That figure covers many industries, not coating machines alone, but it highlights the cost of overlooking material compatibility. Ask suppliers for test methods and documented results, then compare them with your process conditions. A specification can still miss something. Review it after a change in formulation, cleaning practice, or production speed.
How to Choose the Right Coating Machine Parts?
Material compatibility is a practical starting point. A roller, seal, or pump component may contact coating, cleaning fluids, and moisture during one shift. Check the material data against every liquid it will encounter, not just the main coating. Look for swelling, softening, corrosion, or surface changes after exposure. Small details matter. A short compatibility test under real operating conditions can reveal problems that a specification sheet may not predict.
Wear resistance depends on more than hardness. Abrasive pigments, repeated web contact, pressure, and cleaning methods all affect part life. A harder doctor blade may resist abrasion, yet damage a delicate roll surface. Match the part to the actual contact and load. Inspect wear patterns regularly; uneven marks can point to alignment or pressure issues, not simply poor material. Not always.
Service life also depends on temperature, speed, and maintenance. Record how long parts run before coating defects or dimensional changes appear. Compare those observations across similar production jobs, while noting changes in coating and cleaning routines. There is no universal replacement interval, and estimates can be wrong. Review technical data with a qualified parts supplier, then verify the choice in a controlled trial before changing multiple machine positions.
| Machine Part | Typical Material Options | Compatibility Considerations | Main Wear or Failure Mode | Selection Guidance | Indicative Service-Life Planning Range |
|---|---|---|---|---|---|
| Metering / doctor blade | Stainless steel; spring steel; polymer blade materials such as polyurethane | Check coating chemistry, temperature, solvent exposure, and whether the blade material can tolerate the applied pressure. | Edge wear, corrosion, chipping, deformation, or scoring from particles. | Use a corrosion-resistant grade for chemically aggressive liquids. For delicate substrates, consider a suitable polymer blade and verify its solvent compatibility. | About 100–1,000 operating hours for replaceable blades; highly dependent on coating abrasiveness, blade loading, and setup. |
| Coating or transfer roller | Steel or aluminum core with rubber, polyurethane, or other engineered elastomer covering | Confirm resistance to the coating liquid, cleaning solvent, operating temperature, and any swelling or softening risk. | Cover wear, swelling, cracking, surface glazing, and loss of profile or hardness. | Choose cover hardness and surface finish for the required film transfer and substrate. Test elastomer compatibility with the actual coating and cleaning fluids. | About 5,000–20,000 operating hours before major reconditioning or replacement in many routine applications. |
| Feed or circulation pump wetted parts | Stainless steel; compatible engineering plastics; ceramic or hard-coated surfaces for selected duties | Match wetted materials to pH, solvents, temperature, solids content, and cleaning chemicals. Check seals separately. | Abrasive erosion, corrosion, cavitation, and wear at clearances or impeller surfaces. | For abrasive suspensions, prioritize erosion resistance and suitable clearances. For corrosive fluids, verify the exact alloy or polymer against the full chemical mixture. | About 4,000–15,000 operating hours for major wetted components under routine service; abrasive or corrosive duty can shorten life substantially. |
| Pump mechanical seal | Carbon or silicon-carbide faces; elastomer secondary seals such as EPDM or FKM, selected for the fluid | Seal faces and elastomers must be compatible with the coating, flushing fluid, cleaning agents, pressure, and temperature. | Face wear, dry running, chemical attack, thermal damage, or leakage caused by solids. | Use seal-face materials suited to solids and lubrication conditions. Select the elastomer by checking a chemical compatibility chart for the exact fluid and temperature. | About 2,000–8,000 operating hours in suitable service; dry running, poor flushing, or abrasive solids may reduce this range. |
| Spray nozzle or applicator orifice | Stainless steel; carbide; ceramic; compatible polymer materials for selected low-pressure applications | Consider coating viscosity, solids size, solvent or water chemistry, pressure, and cleaning method. | Orifice enlargement, blockage, erosion, corrosion, and spray-pattern distortion. | For abrasive coatings, consider wear-resistant carbide or ceramic. Ensure the material and nozzle geometry are appropriate for the coating and required flow rate. | About 500–5,000 operating hours; abrasive formulations and frequent cleaning can change the interval considerably. |
| Gaskets and O-rings | EPDM, FKM, PTFE, or other fluid-compatible elastomers and polymers | Compatibility depends on the exact chemical blend, concentration, temperature, pressure, and cleaning cycle. | Swelling, shrinkage, hardening, cracking, extrusion, or compression set. | Do not select by material name alone. Check a chemical compatibility chart and confirm the operating temperature and pressure limits. | About 1,000–8,000 operating hours, or replacement at scheduled maintenance; chemical exposure and compression conditions are decisive. |
| Roller bearings | Hardened bearing steel; corrosion-resistant bearing steel or suitable sealed bearing assemblies | Assess washdown exposure, coating contamination, ambient humidity, operating speed, load, and lubricant compatibility. | Fatigue, contamination, corrosion, lubricant breakdown, and overheating. | Use effective sealing and appropriate lubrication where coating or cleaning fluids may enter the bearing. Confirm load and speed ratings against the machine duty. | About 10,000–40,000 operating hours under appropriate load, alignment, lubrication, and contamination control. |
Before ordering a coating machine part, measure the old component and compare it with the machine drawing. Check its length, outside diameter, bore size, and mounting-hole spacing with a caliper or steel rule. A few millimeters can shift a roller, create uneven coating, or strain a bearing. Measure twice. Record the units and stated tolerances. For threaded fittings, confirm thread type, pitch, and gender; similar-looking connections may not seal correctly. Inspect sealing faces and gasket dimensions, especially on fluid or compressed-air lines. This is easy to overlook.
Then compare the part with the machine’s operating specifications. Check rated speed, temperature range, pressure, voltage, and material compatibility where relevant. A component may fit physically yet fail under the machine’s actual load or operating conditions. Don’t rely on a photo alone. Use the equipment manual or technical drawing, and ask technical support to clarify missing dimensions or connection details. A rushed estimate can feel efficient, but it is still a guess. If measurements conflict, pause and verify them before installation. Keep a note of the confirmed dimensions and specifications so future replacements are easier to check.
A coating machine part can look inexpensive until it causes streaks, leaks, or an unplanned line stop. Compare suppliers on documented quality: material certificates, dimensional inspection, batch traceability, and clear defect-handling procedures. For rollers, check runout and surface finish; for doctor blades, confirm edge consistency and compatibility with the coating process. Ask how inspection results are recorded, not just whether inspection happens. Small details matter.
Availability deserves equal weight. Request standard and expedited lead times, local stock levels, and written notice of part changes. Then compare total ownership cost: purchase price, freight, installation labor, expected service life, cleaning needs, and downtime exposure. The U.S. Department of Energy’s Operations & Maintenance Best Practices Guide reports that predictive maintenance can save 8–12% compared with preventive maintenance. That figure is a maintenance-program benchmark, not a promise that any replacement part will deliver the same savings. Track actual failures and delivery performance over several orders; a supplier’s estimate may miss real operating conditions. A cheap spare that arrives late is not cheap.
This site uses cookies. By continuing to browse the site, you are agreeing to our use of cookies.
OKLearn moreWe may request cookies to be set on your device. We use cookies to let us know when you visit our websites, how you interact with us, to enrich your user experience, and to customize your relationship with our website.
Click on the different category headings to find out more. You can also change some of your preferences. Note that blocking some types of cookies may impact your experience on our websites and the services we are able to offer.
These cookies are strictly necessary to provide you with services available through our website and to use some of its features.
Because these cookies are strictly necessary to deliver the website, refusing them will have impact how our site functions. You always can block or delete cookies by changing your browser settings and force blocking all cookies on this website. But this will always prompt you to accept/refuse cookies when revisiting our site.
We fully respect if you want to refuse cookies but to avoid asking you again and again kindly allow us to store a cookie for that. You are free to opt out any time or opt in for other cookies to get a better experience. If you refuse cookies we will remove all set cookies in our domain.
We provide you with a list of stored cookies on your computer in our domain so you can check what we stored. Due to security reasons we are not able to show or modify cookies from other domains. You can check these in your browser security settings.
We also use different external services like Google Webfonts, Google Maps, and external Video providers. Since these providers may collect personal data like your IP address we allow you to block them here. Please be aware that this might heavily reduce the functionality and appearance of our site. Changes will take effect once you reload the page.
Google Webfont Settings:
Google Map Settings:
Google reCaptcha Settings:
Vimeo and Youtube video embeds: