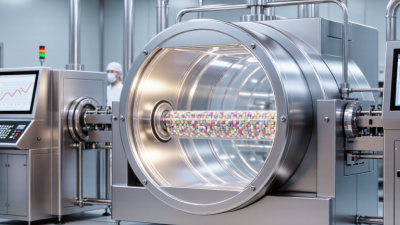
Optimizing the tablet coating process is not merely a matter of increasing spray speed. It requires controlled interaction between formulation, equipment, airflow, temperature, and operator decisions. A tablet may leave the pan glossy, yet still contain weak adhesion, uneven color, or hidden moisture variation. Small changes matter. A blocked nozzle can create rough patches within minutes.
Professor James W. McGinity, a recognized pharmaceutical coating researcher, described film coating as “a complex process involving simultaneous heat and mass transfer.” That principle remains practical today. The FDA’s Process Validation Guidance recommends linking process parameters with critical quality attributes through continued process verification. ICH Q8(R2) also supports a science-based design space, rather than relying on fixed settings alone. Industry data points in the same direction. Grand View Research’s pharmaceutical excipients reports identify sustained demand for functional coatings, driven by modified release, taste masking, and product stability. Mordor Intelligence’s tablet coating equipment analysis likewise highlights automation and process control as important market trends.
In practice, optimization begins with measurable evidence. Track inlet temperature, exhaust temperature, spray rate, atomization pressure, pan speed, and weight gain. Examine tablets, not only dashboards. A coating may look uniform under bright light but fail friability testing later. That is the uncomfortable part: operators often optimize one result while weakening another. The better approach combines design of experiments, in-process inspection, and realistic scale-up trials. Perfect control is unlikely. Repeatable control is achievable.
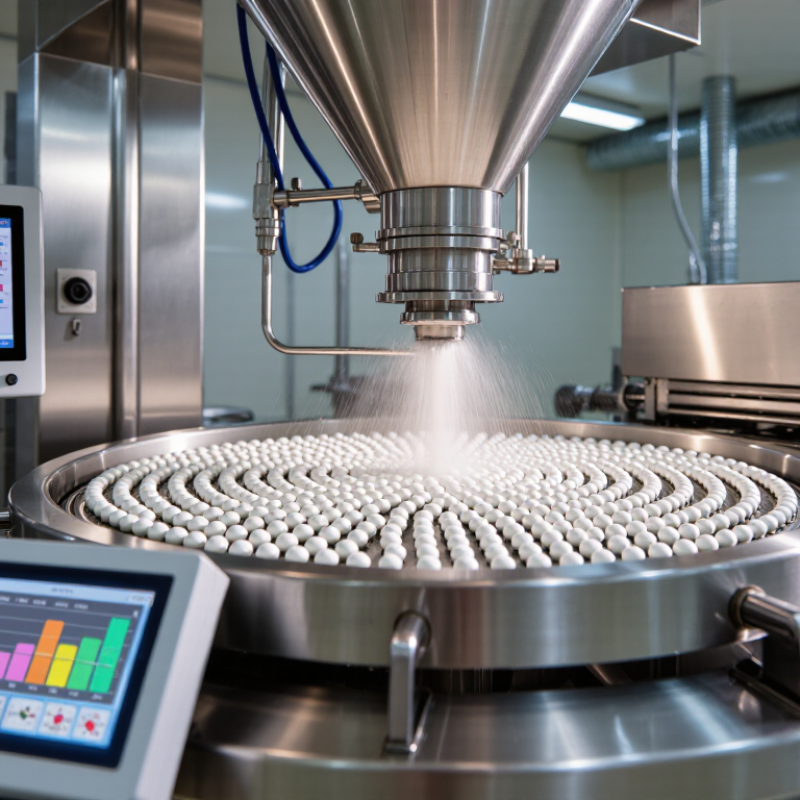
Tablet coating is a controlled film-forming operation, not simply a spraying step. The core variables include pan speed, inlet temperature, airflow, spray rate, and atomization pressure. Each variable affects drying, tablet movement, and surface appearance. A sound process begins with the tablet core. It should have suitable hardness, low friability, and a consistent shape. Otherwise, coating defects may reflect compression problems rather than the coating formula. This distinction is easy to miss.
During development, establish a practical operating window instead of chasing one perfect setting. Monitor tablet-bed temperature, exhaust conditions, spray pattern, and weight gain. Calibrated instruments improve data reliability. Check samples for sticking, twinning, color variation, edge erosion, and roughness. A stable spray should create even coverage without visible overwetting. If defects appear, change one major parameter at a time. Multiple adjustments can hide the real cause. Experience helps, but records protect the process from memory-based decisions. A smooth finish is useful, yet it does not always prove uniform coating performance.
Tips: Keep the spray gun aligned with the moving tablet bed. Confirm nozzle cleanliness before each run. Increase spray rate gradually. Watch the exhaust air, not only the inlet display. Allow enough mixing time after spraying. Review failed batches honestly; the first explanation may be wrong. Small changes in airflow can alter drying behavior, especially with different tablet loads. Document every adjustment, including settings that seemed unimportant.
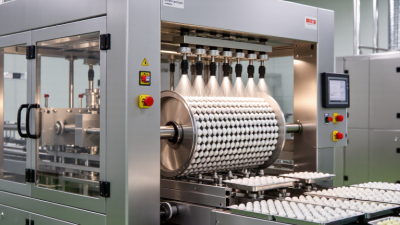
Preparation begins with the tablet core. Check hardness, friability, moisture, and weight variation before coating. A weak core can chip inside the pan. Excess moisture may create sticking, roughness, or delayed drying. FDA’s 2019 Drug Shortages Task Force report linked 62% of shortages to manufacturing and product-quality problems. This supports tighter preparation controls, not faster production.
Materials need consistent particle size, solids content, viscosity, and suspension stability. Record mixing time and inspect the coating liquid for sediment. Equipment preparation matters equally. Verify pan cleanliness, spray-nozzle alignment, air temperature, airflow, and exhaust balance. A calibrated scale helps confirm coating weight gain. Keep the spray distance stable. Small changes can produce large surface defects. I have seen teams adjust spray rate before checking inlet air. That is often the wrong correction.
Tips: Start with a small engineering trial. Measure tablet temperature, atomization pressure, spray rate, and weight gain every few minutes. Keep a simple batch map with observations, not only numbers. Allow enough drying time between checks. Do not assume a smooth appearance proves uniform coating. The first trial may remain imperfect. Review defects by location, timing, and equipment setting. Use FDA Process Validation guidance and ICH Q8 principles to connect material attributes with critical process parameters.
How to Optimize the Tablet Coating Process?
Setting Critical Coating Parameters
Tablet coating becomes reliable when critical parameters are measurable, controlled, and linked to product quality. Start with coating weight gain. Published pharmaceutical manufacturing studies commonly report 2–5% weight gain for immediate-release film coatings, though the target depends on formulation and performance requirements. ICH Q8(R2) recommends connecting process parameters with critical quality attributes, not selecting settings by habit.
Keep product temperature stable, often within 40–50°C for aqueous systems. Excess heat can cause spray-drying and rough surfaces. Low temperature may create sticking. Spray rate must match drying capacity. In practice, operators should monitor inlet air temperature, exhaust temperature, airflow, atomization pressure, pan speed, and suspension solids. Small changes matter.
Use a documented design space, as recommended by FDA’s Process Validation guidance. Record tablet-bed appearance, weight gain, and moisture during development batches. A 2021 ISPE oral solid dosage guide also emphasizes equipment scale-up and airflow evaluation. However, reported ranges are not universal. A setting that works on one perforated pan may fail on another. I would not pretend that a smooth surface proves process control. Coating thickness can still vary across the batch. Check samples from different pan locations, review spray-pattern coverage, and challenge the process with realistic operating limits. Do not guess.
This representative aqueous film-coating profile shows how product temperature, exhaust temperature, and spray rate can be coordinated during preheating, spraying, and cooling. A product-temperature range of approximately 35–45°C is commonly used as a starting window for many aqueous coating systems, but the final settings should be confirmed through formulation trials, tablet-bed monitoring, and coating-quality tests.
How to Optimize the Tablet Coating Process?
Monitoring Spray, Drying, and Pan Conditions
A reliable coating process begins with watching the spray, not merely setting its rate. Check nozzle pattern, atomization pressure, liquid temperature, and spray distance during the run. A stable pattern should wet tablet surfaces evenly without creating visible droplets. Excessive spray can produce picking, twinning, or rough patches. Insufficient spray may leave weak color coverage and exposed edges.
Drying conditions need equal attention. Track inlet air temperature, outlet temperature, airflow, and exhaust humidity at regular intervals. The outlet temperature often reveals how much moisture the tablet bed is releasing. If it rises suddenly, the spray rate may be too low, or the bed may be drying too quickly. If it remains unusually low, overwetting could be developing. Small samples can confirm what instruments suggest. They should be checked for weight gain, surface texture, hardness, and residual moisture.
Pan conditions shape the final result. Monitor pan speed, tablet bed depth, baffle performance, and exhaust balance. Tablets should cascade smoothly rather than slide as a heavy mass. Uneven movement can create coating differences, even when spray settings look correct. In practice, I have found that operators sometimes trust preset values too much. That is a mistake worth revisiting. Room humidity, tablet shape, and coating suspension behavior can shift between batches. Record these changes, investigate unexpected trends, and adjust one variable at a time. The process is rarely perfect.
| Process Area | Monitoring Dimension | Recommended Operating Range | Illustrative Batch Reading | Control Rationale | Status |
|---|---|---|---|---|---|
| Spray System Conditions | |||||
| Spray | Coating Suspension Solids | 10–20% w/w | 15.0% w/w | Maintains a practical balance between coating efficiency, suspension stability, and atomization quality. | Within target |
| Spray | Suspension Viscosity | 100–500 mPa·s at process temperature | 280 mPa·s | Excessive viscosity can cause poor atomization, nozzle blockage, and uneven film distribution. | Within target |
| Spray | Spray Rate | 6–12 g/min per spray gun | 8.5 g/min per spray gun | Controls the liquid load applied to the tablet bed and should be adjusted together with drying capacity. | Within target |
| Spray | Atomizing Air Pressure | 1.5–2.5 bar | 2.0 bar | Supports fine and consistent droplets while limiting excessive spray mist and over-drying. | Within target |
| Spray | Nozzle-to-Bed Distance | 20–30 cm | 25 cm | Helps provide uniform spray coverage and reduces localized overwetting or spray drying before deposition. | Within target |
| Spray | Nozzle Condition | Clean, unobstructed, and producing a symmetrical spray pattern | Pattern symmetrical; no visible blockage | Partial blockage can create coating variability, edge defects, and non-uniform tablet appearance. | Acceptable |
| Spray | Spray Gun Alignment | Parallel to the tablet bed with overlapping spray fans | Aligned; spray fans overlap by approximately 10% | Correct alignment improves coverage across the moving tablet bed and reduces localized coating differences. | Acceptable |
| Drying and Air Management | |||||
| Drying | Inlet Air Temperature | 55–70°C | 62°C | Provides sufficient drying energy while helping protect heat-sensitive coating components and active ingredients. | Within target |
| Drying | Outlet Air Temperature | 38–45°C | 41°C | Reflects the balance between evaporative load and drying capacity; sudden changes may indicate process instability. | Within target |
| Drying | Inlet Air Relative Humidity | Below 30% RH | 24% RH | Lower humidity improves moisture removal and reduces the risk of tackiness or prolonged drying. | Within target |
| Drying | Airflow Rate | 1,200–1,800 m³/h | 1,500 m³/h | Maintains effective tablet movement and solvent or water evaporation without excessive attrition. | Within target |
| Drying | Exhaust Airflow Balance | Stable negative pressure; typically −5 to −15 Pa | −10 Pa | Stable pressure supports controlled air movement and minimizes uncontrolled dust or vapor release. | Stable |
| Drying | Tablet Bed Moisture Trend | Gradual decrease with no sudden moisture spikes | Decreased from 3.8% to 1.9% during coating | A controlled moisture trend indicates that spray application and drying are adequately balanced. | Stable |
| Drying | Final Tablet Moisture | Product-specific specification; example: 1.0–2.5% w/w | 1.7% w/w | Final moisture should meet the validated product specification and support acceptable stability and mechanical strength. | Within target |
| Pan and Tablet-Bed Conditions | |||||
| Pan | Pan Speed | 6–12 rpm | 9 rpm | Determines tablet cascading behavior, residence time under the spray zone, and exposure to drying air. | Within target |
| Pan | Pan Fill Level | Approximately 50–75% of usable pan volume | 65% of usable volume | Provides sufficient tablet movement and mixing without overloading the pan or reducing spray access. | Within target |
| Pan | Tablet Bed Temperature | 35–45°C, depending on formulation sensitivity | 39°C | Helps maintain coating coalescence while limiting overwetting, sticking, and thermal stress. | Within target |
| Pan | Tablet Bed Mixing Quality | Continuous cascading with no dead zones | Uniform cascading observed | Consistent movement is essential for uniform exposure to the spray zone and drying air. | Acceptable |
| Pan | Tablet Chipping or Edge Damage | Not more than 0.5% visual defects | 0.2% observed during in-process inspection | High mechanical stress, excessive pan speed, or insufficient tablet strength can increase edge damage. | Acceptable |
| Pan | Tablet Sticking or Picking | No persistent sticking or picking | Minor transient sticking observed | Review spray rate, bed temperature, drying airflow, and suspension properties if sticking persists. | Monitor |
| In-Process Quality and Optimization Indicators | |||||
| Quality | Weight Gain | Product-specific target; example: 3–5% w/w | 4.1% w/w | Confirms the amount of coating deposited and should be evaluated together with appearance and performance results. | Within target |
| Quality | Coating Uniformity | Relative standard deviation typically not more than 5% | 3.2% relative standard deviation | Indicates consistent coating distribution across sampled tablets when tested by a validated method. | Within target |
| Quality | Surface Appearance | Smooth, continuous film with consistent color and gloss | Smooth surface; no visible cracks or roughness | Visual defects may indicate poor atomization, excessive spray rate, inadequate drying, or improper tablet movement. | Pass |
| Quality | Coating Defect Rate | Less than 1.0% of inspected tablets | 0.4% of inspected tablets | Tracking defect frequency supports early detection of process drift and helps identify corrective actions. | Acceptable |
| Optimization | Process Capability Review | Critical parameters remain within validated ranges | All critical readings within range; one transient sticking event | Trend data should be reviewed after each batch to distinguish isolated events from recurring process behavior. | Review trend |
Note: The operating ranges shown are representative process-development values. Final limits should be established and validated for the specific tablet formulation, coating system, equipment configuration, and regulatory requirements.
Quality control begins before the coating pan starts. In my experience, stable core tablets produce more reliable coating results. Check tablet hardness, friability, moisture, and weight variation before spraying. Record these values clearly. Small changes can become visible defects later.
During coating, monitor inlet temperature, exhaust temperature, pan speed, spray rate, atomization pressure, and airflow. Keep each parameter within an approved operating range. Do not adjust several settings at once. That makes the real cause difficult to identify. Examine tablets at regular intervals for picking, twinning, roughness, color variation, and logo bridging. Measure weight gain and coating thickness during the run. A clean, representative sample matters.
Process optimization should use trends, not isolated results. Compare spray performance, drying capacity, and appearance data across batches. If defects increase near the end, the bed may be too wet or the spray pattern may be uneven. Check nozzle alignment and airflow distribution before changing the formulation. Dissolution testing must confirm that visual improvement does not reduce product performance. Environmental conditions also deserve attention, especially room humidity and temperature.
Not every adjustment improves the process. A faster spray rate may shorten production time but increase sticking. One weakness in many investigations is relying too heavily on final testing. In-process observations often reveal problems earlier. Document deviations honestly, including failed trials. That record supports better decisions and safer, more consistent manufacturing.
This site uses cookies. By continuing to browse the site, you are agreeing to our use of cookies.
OKLearn moreWe may request cookies to be set on your device. We use cookies to let us know when you visit our websites, how you interact with us, to enrich your user experience, and to customize your relationship with our website.
Click on the different category headings to find out more. You can also change some of your preferences. Note that blocking some types of cookies may impact your experience on our websites and the services we are able to offer.
These cookies are strictly necessary to provide you with services available through our website and to use some of its features.
Because these cookies are strictly necessary to deliver the website, refusing them will have impact how our site functions. You always can block or delete cookies by changing your browser settings and force blocking all cookies on this website. But this will always prompt you to accept/refuse cookies when revisiting our site.
We fully respect if you want to refuse cookies but to avoid asking you again and again kindly allow us to store a cookie for that. You are free to opt out any time or opt in for other cookies to get a better experience. If you refuse cookies we will remove all set cookies in our domain.
We provide you with a list of stored cookies on your computer in our domain so you can check what we stored. Due to security reasons we are not able to show or modify cookies from other domains. You can check these in your browser security settings.
We also use different external services like Google Webfonts, Google Maps, and external Video providers. Since these providers may collect personal data like your IP address we allow you to block them here. Please be aware that this might heavily reduce the functionality and appearance of our site. Changes will take effect once you reload the page.
Google Webfont Settings:
Google Map Settings:
Google reCaptcha Settings:
Vimeo and Youtube video embeds: