Top 10 Aluminium Die Casting Machine Manufacturers Worldwide
An Aluminium Die Casting Machine is more than a press with a large clamping force. It combines metal delivery, injection, tooling, cooling, and controls in one demanding production system. In automotive, electronics, and appliance manufacturing, small process differences can affect part consistency, surface finish, cycle time, and scrap. A machine that looks impressive on a specification sheet may still be a poor fit for a particular component. That distinction matters.
Casting specialist Professor Diran Apelian’s work on materials processing offers a useful principle, paraphrased here: reliable castings depend on controlling the whole process, not horsepower alone. Buyers should weigh shot performance, repeatability, automation options, maintenance access, and technical support alongside machine capacity. The details are tangible: how steadily the machine fills a thin-walled cavity, how quickly operators can inspect a component, and how easily a tool change fits the production schedule.
This guide introduces ten manufacturers active in the global Aluminium Die Casting Machine market. It compares their capabilities and product focus without treating every machine as interchangeable. Company portfolios, specifications, and service networks can change, so current manufacturer information should be checked before making a purchasing decision. No ranking is perfect. That is worth admitting. A machine suited to high-volume automotive parts may not suit a smaller foundry or a different alloy. The aim is a practical starting point: clearer questions, sharper comparisons, and fewer assumptions when evaluating suppliers.
Understanding Aluminium Die Casting Machines and Their Role
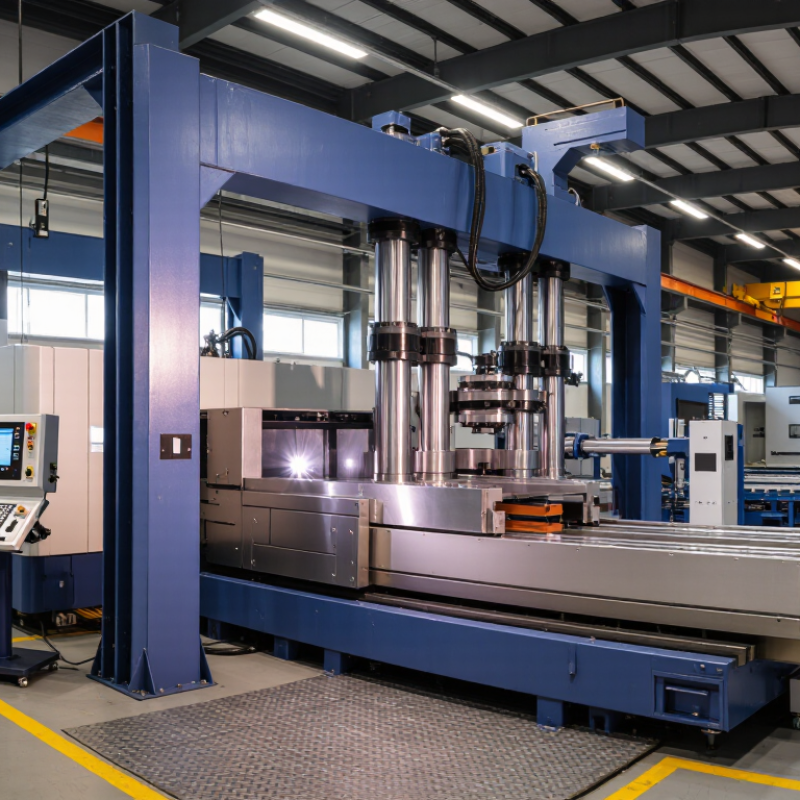
An aluminium die casting machine injects molten metal into a steel die under pressure. The metal fills narrow ribs, bosses, and thin walls before it solidifies. This makes the process useful for producing complex, repeatable parts, including housings and structural components. The machine’s clamping force must resist the metal pressure, while its injection system controls speed and fill. Temperature matters, too. A cold die can cause incomplete filling; excessive heat may lengthen cooling time and shorten die life.
Machine selection affects more than output per hour. Shot size, tie-bar spacing, platen dimensions, and control precision must match the component and die. The U.S. Department of Energy’s Vehicle Technologies Office reports that reducing vehicle weight by 10% can improve fuel economy by 6–8%. Aluminium castings can support lightweighting, but the machine alone cannot guarantee a lighter, stronger part. Small details matter. Poor venting or unstable melt temperature can create porosity and scrap. A faster cycle is not automatically a better one; production teams still need to balance quality, energy use, and tool wear. On a real shop floor, that balance can be less tidy than a machine specification suggests.
Top 10 Aluminium Die Casting Machine Manufacturers Worldwide - Understanding Aluminium Die Casting Machines and Their Role
A non-branded guide to 10 machine capabilities and selection factors. It is not a verified ranking of manufacturers.
| No. | Capability or Selection Factor | Factual Context | Why It Matters |
| 1 | Cold-chamber injection system | Aluminium die casting commonly uses a cold-chamber process: molten metal is transferred into a separate shot sleeve before injection. | The system must accommodate the alloy, shot size, and required production cycle. |
| 2 | Clamping force | Required clamping force depends on factors including the projected area of the casting and the pressure applied during filling. | Adequate force helps keep the die closed and limit flash; selection should be based on the specific die and process. |
| 3 | Shot capacity | Shot capacity refers to the amount of metal the injection system can deliver in a shot; the required amount includes the casting and the runner system. | The machine must be sized for the part and die layout, with a suitable process window. |
| 4 | Die size and tie-bar spacing | Platen dimensions, tie-bar spacing, and die-height limits define the moulds that can be mounted on a machine. | Checking these dimensions helps ensure the intended die fits and can be installed and operated safely. |
| 5 | Injection control | Modern systems can control injection parameters such as speed and pressure across stages of the shot. | Repeatable control supports consistent filling and helps production teams tune the process for a particular casting. |
| 6 | Vacuum assistance | Vacuum-assisted die casting removes air from the die cavity before or during filling, depending on the system and process design. | It can reduce gas entrapment, but it does not guarantee porosity-free castings; die design and process control remain important. |
| 7 | Automation compatibility | Die casting cells may integrate metal dosing, part extraction, spraying, trimming, and conveying equipment. | Automation can reduce manual handling and support consistent cycle execution when matched to the factory layout and part requirements. |
| 8 | Process monitoring | Machine controls can record process settings and operating data, with available monitoring features varying by configuration. | Recorded data helps operators track production, investigate process variation, and maintain repeatable settings. |
| 9 | Energy and hydraulic system | Machine energy use depends on the drive system, operating cycle, auxiliary equipment, and production conditions. | Comparing energy data under equivalent operating conditions gives a more useful basis for evaluating running costs. |
| 10 | Service and spare-parts support | Maintenance needs depend on machine design, usage, and operating environment; access to technical support and replacement parts varies by supplier and location. | Evaluating service response, training, maintenance requirements, and parts availability can help reduce unplanned downtime. |
Criteria for Ranking Global Machine Manufacturers
Ranking global aluminium die casting machine manufacturers requires more than comparing catalogue figures. A sound review checks clamping force, shot capacity, tie-bar spacing, and compatible alloy temperatures against real part requirements. These details determine whether a machine can handle a thin-walled housing or a heavier structural component. Performance evidence matters too. Reviewers should compare cycle stability, shot-to-shot repeatability, scrap rates, and energy use under similar production conditions. A fast cycle means little if parts show porosity or dimensions drift across a shift. Numbers need context.
Credible rankings also weigh engineering support and long-term service. Factory visits, documented customer references, spare-part availability, operator training, and response times can reveal strengths that brochures omit. Independent test records and clearly dated specifications make comparisons easier to verify. Safety features and maintenance access deserve attention, since technicians work around hot metal, moving platens, and hydraulic systems. Scores should state how technical performance, service, and reliability are weighted; otherwise, readers cannot tell why one supplier ranks above another. No score is perfect. Regional service coverage and product mix can skew results, while a brief inspection may miss issues that appear after months of operation. A ranking should show its evidence and limits, not pretend every plant needs the same machine.
Profiles of the Top 10 Aluminium Die Casting Machine Manufacturers
Profiles of the top ten aluminium die casting machine manufacturers should compare practical capability, not just headline clamping force. Grand View Research valued the global die-casting market at USD 79.7 billion in 2023 and projected 6.4% annual growth through 2030. The International Energy Agency reported nearly 14 million electric car sales in 2023, supporting demand for lightweight components. These figures indicate market momentum, but they do not prove that every machine supplier will benefit equally.
A useful profile examines machine size, shot-control precision, automation options, energy use, and access to local technical service. Some manufacturers focus on high-pressure cells for automotive structural parts; others serve smaller components or flexible production lines. Details matter. Compare cycle stability and metal yield under real operating conditions, not only brochure specifications. Ask how quickly spare parts arrive, and whether operators receive hands-on commissioning support. A ranking can still miss regional service differences or customer-specific needs. Market estimates also vary by methodology, so figures should be treated as indicators, not guarantees. These profiles therefore assess stated capabilities alongside practical questions buyers can verify.
Clamping force is a key specification used to compare aluminium die casting machines. The ranges shown are representative capacity bands found across the industry, not rankings or data for specific manufacturers; available capacities vary by machine and supplier.
Comparing Technologies, Capacities, and Production Strengths
Aluminium die casting machines differ in more than clamping force. Most use cold-chamber systems, where molten metal enters a separate shot sleeve before injection. This setup suits aluminium’s high pouring temperature and supports repeatable, high-pressure filling. Modern controls can adjust shot speed and pressure in stages, helping reduce porosity in thin walls and complex ribs. Small changes matter.
Machine capacity is often stated by clamping force, but tonnage alone tells little. A large frame may be inefficient for a compact component, while an undersized machine can struggle with projected area and cavity pressure. Buyers should compare tie-bar spacing, platen dimensions, shot weight, and die thickness alongside cycle time. The numbers need context.
Production strengths depend on the full cell: furnace, ladling method, die temperature control, extraction, trimming, and inspection. Vacuum-assisted filling can improve results for parts requiring tighter internal quality, but it adds equipment and process checks. Automation helps sustain output across shifts, though poorly tuned handling can create its own stoppages. There is no perfect configuration. A useful comparison asks how steadily each machine holds settings during a real production run, not just what its brochure promises. I would still verify sample parts and maintenance access before choosing.
How to Select a Manufacturer for Your Casting Requirements
Selecting an aluminium die casting machine manufacturer starts with the part, not the machine catalogue. Share the alloy, casting weight, projected area, required output, and drawings for your largest components. These details help determine clamping force, shot capacity, and whether a cold-chamber system suits the job. Check platen dimensions and tie-bar spacing too. A machine may have enough tonnage yet still not fit your die.
Ask how the manufacturer validates performance. Request cycle-time assumptions, shot repeatability data, energy estimates, and a clear factory acceptance test plan. A sample casting can reveal issues that a brochure cannot: porosity near a thick rib, flash along a parting line, or inconsistent fill at the end of a long flow path. Ask who will help tune the process after installation. That matters.
Service details deserve equal attention. Confirm technician response times, spare-part availability, training hours, and the controls or automation included in the quoted price. Speak with users running similar alloys and part sizes, if possible. A larger machine can seem reassuring, but it may raise operating costs without improving your castings. I would not decide on price alone. One honest limitation: quoted cycle times may depend on ideal conditions, so ask what changes them in real production.