Material Handling Equipment keeps warehouses, factories, ports, and distribution centers moving. Forklifts lift pallets, conveyors guide cartons, and automated systems reduce repetitive travel. When one component fails, a loading dock can become crowded within minutes. Small delays become expensive quickly.
This guide examines leading manufacturers worldwide, including Toyota Material Handling, KION, Jungheinrich, Crown, Hyster-Yale, Daifuku, and SSI SCHAEFER. The list does not depend on brand popularity alone. It considers product reliability, operator safety, service coverage, automation expertise, energy efficiency, and replacement-parts availability. These factors matter more than a polished brochure. A reliable forklift with accessible maintenance support can outperform a smarter machine stranded without technicians.
Real warehouse conditions remain difficult. A cold storage site needs equipment that tolerates low temperatures and limited visibility. A busy retail facility may prioritize turning radius, battery charging speed, and noise control. Manufacturers also differ across regions. Their dealer networks, training programs, warranty terms, and software integrations can change the ownership experience. That detail is easy to overlook.
The strongest companies usually combine engineering depth with long-term customer support. Yet no manufacturer is perfect. Some systems cost more upfront, while others require complex integration or specialized maintenance. Buyers should verify performance data through independent testing, customer references, technical documents, and local service records. Rankings can also shift as technologies develop. This overview offers a practical starting point, not a final verdict, for comparing the world’s top Material Handling Equipment manufacturers.
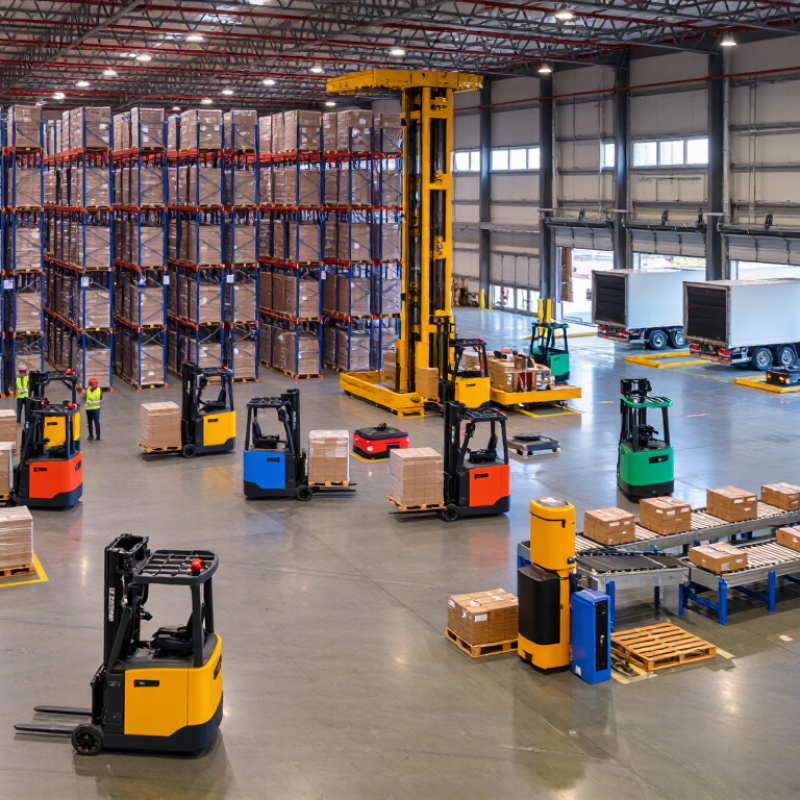
Material handling equipment includes machines and systems used to move, store, protect, and control goods. It covers conveyors, forklifts, pallet trucks, lifts, cranes, shelving, and automated storage equipment. These tools connect receiving docks, production areas, warehouses, and shipping stations. Without them, even a well-designed facility can become slow and unsafe.
The equipment reduces manual lifting, shortens travel distances, and improves inventory flow. A conveyor can move cartons between work zones while workers inspect labels or scan records. A suitable lift can place heavy pallets onto upper racks with controlled movement. Storage systems also use vertical space, which matters when floor area is expensive. In my experience, the right choice depends on load weight, aisle width, product shape, traffic levels, and operator skill.
Manufacturers worldwide develop equipment for different industries and working conditions. However, advanced features do not guarantee better performance. A highly automated system may struggle when product sizes change often. A simple pallet truck may serve a small warehouse more reliably. That assumption needs testing. Maintenance access, battery charging, training, emergency controls, and spare parts should be reviewed before installation. One overlooked detail can stop an entire workflow. Good material handling equipment supports people; it should not force workers to adapt to an impractical design.
Material handling equipment includes machines and systems used to move, lift, store, sort, and control goods across warehouses, factories, distribution centers, and ports. The chart compares representative rated load capacities for widely used equipment categories. Actual capacity varies by model, mast height, attachment, and operating conditions.
Higher-capacity equipment is generally used for heavy pallet movement and industrial storage, while lower-capacity equipment is often selected for order picking, narrow-aisle operations, and automated internal transport. Capacity is only one purchasing factor; safety, energy efficiency, operating height, aisle width, automation level, and total cost of ownership are also important.
Material handling equipment supports movement, storage, picking, and production flow. Conveyors suit high-volume distribution centers and manufacturing lines. Forklifts serve pallet movement, loading docks, and cold-storage areas. Cranes and hoists handle heavy steel, machinery, and engine components. Each category solves a different operational problem.
Automated storage and retrieval systems improve space use and inventory access. Autonomous mobile robots support tote delivery and order picking across structured warehouses.
The MHI 2024 Annual Industry Report found that 55% of surveyed companies planned to increase supply chain technology investment.
Its findings also show rising interest in robotics, automation, and warehouse execution software. These systems can reduce walking time, but they require reliable data and disciplined process design.
Industrial application determines the right equipment. A food facility may prioritize hygienic conveyors and temperature-resistant components. An automotive plant may need overhead handling and precise line-side delivery.
The International Federation of Robotics reported 541,302 industrial robots installed worldwide in 2023, showing continued automation growth.
However, robot adoption does not automatically improve throughput. Poor layout still creates congestion. Human oversight remains important. Report definitions also vary, so direct comparisons can mislead.
In practice, equipment selection should consider load weight, aisle width, travel distance, safety controls, maintenance access, and operator training. Small design errors become expensive quickly.
Leading Material Handling Equipment Manufacturers Worldwide
The global material handling equipment market is expanding with warehouse automation, labor shortages, and e-commerce demand. Fortune Business Insights valued the market at about USD 216 billion in 2023. Its report projects continued growth through 2030, although regional forecasts differ. Leading manufacturers are responding with forklifts, conveyors, automated storage systems, cranes, and mobile robots.
MHI’s 2024 Annual Industry Report found that 55% of supply chain professionals planned to increase technology investment. This figure reflects stronger demand for connected equipment and measurable productivity. Reliable manufacturers now provide sensors, fleet dashboards, battery monitoring, and maintenance alerts. These features help operators track idle time, collision risks, energy use, and equipment availability. Practical experience still matters. A smooth dashboard cannot repair poor aisle design or weak operator training.
The strongest manufacturers also focus on safety, service coverage, and lifecycle cost. Deloitte’s 2024 manufacturing research identified automation and digital technologies as major investment priorities. However, adoption is not always simple. A compact warehouse may need narrow-aisle trucks, while a cold-storage site requires different batteries, controls, and protective materials. Numbers can mislead. A high automation rate may hide expensive integration work, software delays, or difficult maintenance access. Buyers should examine independent testing, spare-parts response times, warranty terms, and documented workplace performance. The best supplier is not always the largest. It is the one that fits the load, floor conditions, workforce, and operating hours.
| Equipment Segment | Common Equipment Types | Typical Rated Capacity | Typical Lift or Operating Height | Common Power Sources | Primary Applications | Relevant International Standards |
|---|---|---|---|---|---|---|
| Counterbalance Forklifts | Electric, diesel, and liquefied-gas forklifts | Approximately 1.0–16.0 tonnes | About 3–7 metres for standard warehouse and industrial configurations | Lead-acid battery, lithium-ion battery, diesel, or liquefied petroleum gas | Loading docks, manufacturing plants, distribution centres, and outdoor yards | ISO 3691-1; ISO 5053-1; ISO 22915 series |
| Reach Trucks | Stand-up reach trucks and double-deep reach trucks | Approximately 1.0–2.5 tonnes | Commonly 6–13 metres in high-density storage areas | Rechargeable electric battery systems | High-bay warehouses, pallet-rack storage, and narrow aisles | ISO 3691-1; ISO 5053-1; ISO 22915 series |
| Electric Pallet Trucks | Walkie pallet trucks, platform pallet trucks, and rider pallet trucks | Approximately 1.5–3.0 tonnes | Floor-level transport with low-height fork lifting, generally below 0.3 metres | Lead-acid or lithium-ion battery | Horizontal pallet movement, order staging, and truck loading | ISO 3691-1; EN 1757-1; ISO 5053-1 |
| Manual Pallet Trucks | Standard hand pallet trucks, low-profile models, and weighing pallet trucks | Commonly 2.0–3.0 tonnes | Typical lifting range of approximately 75–200 millimetres | Manual hydraulic operation | Short-distance pallet handling, retail backrooms, and small warehouses | EN 1757-1; ISO 5053-1 |
| Electric Stackers | Walk-behind stackers, straddle stackers, and counterbalanced stackers | Approximately 0.8–2.0 tonnes | Commonly 2–5.5 metres | Rechargeable electric battery | Light-duty pallet storage, production areas, and small distribution facilities | ISO 3691-1; ISO 5053-1; ISO 22915 series |
| Order Pickers | Low-level, medium-level, and high-level order-picking trucks | Load platforms commonly support approximately 1.0–1.5 tonnes | Platform heights range from floor level to more than 10 metres, depending on type | Electric battery | Piece-picking operations, e-commerce fulfilment, and case-picking warehouses | ISO 3691-1; ISO 5053-1; ISO 22915 series |
| Automated Guided Vehicles | Automated pallet movers, tugger vehicles, and unit-load vehicles | Commonly 0.5–2.0 tonnes for warehouse applications; higher capacities are available | Primarily floor-level movement; some systems interface with lifts or automated storage equipment | Lead-acid, lithium-ion, or other rechargeable battery systems | Repetitive transport between receiving, storage, production, and shipping areas | ISO 3691-4; ISO 5053-1; ISO 12100 |
| Automated Storage and Retrieval Systems | Unit-load cranes, mini-load cranes, shuttle systems, and vertical lift modules | System-dependent; commonly handles individual loads from tens of kilograms to several tonnes | Storage structures may exceed 20 metres in high-bay applications | Electric motors, regenerative drives, and automated control systems | High-density storage, buffer inventory, order fulfilment, and controlled-access storage | ISO 12100; EN 528; ISO 13849-1 |
| Conveyor Systems | Belt, roller, chain, accumulation, and sortation conveyors | Varies widely; generally designed for cartons, totes, pallets, or unit loads | Horizontal, inclined, or multi-level conveying layouts | Electric motors, gear drives, and pneumatic components in selected applications | Parcel handling, production lines, distribution centres, and automated sortation | ISO 12100; ISO 13849-1; applicable regional conveyor safety requirements |
| Industrial Cranes and Hoists | Overhead travelling cranes, gantry cranes, jib cranes, and wire-rope hoists | From below 1 tonne to more than 100 tonnes, depending on crane design | Lift height is determined by building structure, runway design, and application requirements | Electric motors; manual operation is used for selected light-duty equipment | Steel processing, heavy manufacturing, maintenance workshops, and assembly facilities | ISO 4301; ISO 9927; ISO 12480-1 |
| Dock and Loading Equipment | Dock levellers, vehicle restraints, dock shelters, and loading ramps | Typically designed for commercial vehicles and loads from approximately 6–15 tonnes or more | Dock leveller travel commonly accommodates differences of several hundred millimetres between dock and vehicle bed | Hydraulic, mechanical, or electro-hydraulic systems | Vehicle loading bays, warehouses, distribution centres, and manufacturing sites | EN 1398; EN 349; ISO 12100 |
| Storage Racking Systems | Selective pallet racking, drive-in racking, push-back racking, and cantilever racking | Load capacity varies by beam, upright, bay configuration, and floor design | Typical warehouse systems range from approximately 2–12 metres; high-bay systems can be taller | Passive structural systems; automated variants use powered handling equipment | Pallet storage, long-load storage, cold stores, and distribution facilities | EN 15512; EN 15629; EN 15635 |
Top Material Handling Equipment Manufacturers Worldwide?
Material handling equipment is shaped by safety standards, not marketing alone. ISO 3691-4 guides safety for driverless industrial trucks and automated systems. Regional rules may add different testing, guarding, and operator requirements. Reliable manufacturers document load limits, emergency stops, braking distances, and software controls. These details matter beside a warehouse rack, where a small error can injure workers or damage inventory.
Modern facilities increasingly combine automated guided vehicles, autonomous mobile robots, smart conveyors, and sensor-based lifting equipment. Cameras, laser scanners, and proximity sensors help machines detect people and obstacles. Fleet software can balance workloads, monitor battery levels, and record maintenance events. Predictive maintenance is useful when vibration or temperature changes reveal a failing component. Still, data quality remains a weakness. Poorly calibrated sensors can produce confident but unsafe decisions.
Energy efficiency now influences equipment design and purchasing. Lithium-based systems, regenerative braking, modular parts, and quieter drive units can reduce operating costs. Cybersecurity also deserves attention because connected equipment may exchange production data across multiple networks. Human training remains essential, even with advanced automation. Workers need clear procedures for isolation, manual recovery, and unusual loads. No system is flawless. A stronger evaluation compares certified performance with real floor conditions, including narrow aisles, uneven surfaces, seasonal heat, and rushed shift changes.
Choosing top material handling equipment manufacturers requires more than comparing catalog prices. Buyers should examine engineering experience, service capability, safety records, and measurable operating results. The 2024 MHI Annual Industry Report found that 83% of supply chain professionals expect to increase technology and innovation investment. This trend makes supplier evaluation more demanding.
Ask manufacturers for documented uptime, maintenance response times, spare-parts availability, and operator training records. A reliable supplier should explain load capacity, battery performance, turning radius, and floor requirements in practical terms.
Test equipment under real conditions, such as narrow aisles, uneven surfaces, and repeated loading cycles. Ask for evidence. Marketing claims are not enough.
Safety compliance deserves equal attention. The U.S. Occupational Safety and Health Administration emphasizes operator training, inspection, and safe operating procedures for powered industrial trucks. Suppliers should provide clear manuals and inspection guidance. Evaluate total cost over five years, including energy, tires, software, repairs, and downtime. The 2024 MHI report also identifies labor shortages as a continuing operational concern, so automation should reduce repetitive work without creating confusing interfaces. That matters.
A low purchase price can still become expensive. I have seen evaluations focus heavily on equipment speed while overlooking service access and technician coverage. That is a useful warning. Manufacturer references, independent performance data, and transparent warranty terms offer stronger evidence than polished demonstrations. Even experienced buyers should revisit their assumptions before signing.
This site uses cookies. By continuing to browse the site, you are agreeing to our use of cookies.
OKLearn moreWe may request cookies to be set on your device. We use cookies to let us know when you visit our websites, how you interact with us, to enrich your user experience, and to customize your relationship with our website.
Click on the different category headings to find out more. You can also change some of your preferences. Note that blocking some types of cookies may impact your experience on our websites and the services we are able to offer.
These cookies are strictly necessary to provide you with services available through our website and to use some of its features.
Because these cookies are strictly necessary to deliver the website, refusing them will have impact how our site functions. You always can block or delete cookies by changing your browser settings and force blocking all cookies on this website. But this will always prompt you to accept/refuse cookies when revisiting our site.
We fully respect if you want to refuse cookies but to avoid asking you again and again kindly allow us to store a cookie for that. You are free to opt out any time or opt in for other cookies to get a better experience. If you refuse cookies we will remove all set cookies in our domain.
We provide you with a list of stored cookies on your computer in our domain so you can check what we stored. Due to security reasons we are not able to show or modify cookies from other domains. You can check these in your browser security settings.
We also use different external services like Google Webfonts, Google Maps, and external Video providers. Since these providers may collect personal data like your IP address we allow you to block them here. Please be aware that this might heavily reduce the functionality and appearance of our site. Changes will take effect once you reload the page.
Google Webfont Settings:
Google Map Settings:
Google reCaptcha Settings:
Vimeo and Youtube video embeds:
