What Is a Rubber Slitter Cutting Machine?
A Rubber Slitter Cutting Machine cuts wide rubber sheets or rolls into narrower strips. It may use circular blades, rotary knives, or other cutting tools, depending on the material and production setup. The basic idea sounds simple. The details are not.
Rubber can stretch, compress, and shift as a blade passes through it. That makes blade condition, material tension, feed speed, and alignment important to cut quality. A clean edge matters. So does a consistent strip width. In a real workshop, operators may notice small problems first: a fuzzy edge, uneven strips, or rubber tracking slightly off-center. These signs deserve attention, though no single setting works for every compound or thickness.
A transparent note about the expert perspective: Alex Morgan is a fictional composite process engineer, not a verifiable industry authority. The following line is an original illustrative quotation, not a sourced statement: “A good slit begins with stable material, a sharp blade, and settings tested against the actual rubber.” It captures a useful principle, but it should not replace equipment instructions or hands-on testing. There is room for judgment here. Even experienced operators may need to adjust a setup when the rubber changes. This guide explains what the machine does, how its main parts work, and which practical factors buyers and operators should examine before choosing or using one.
Definition and Industrial Role of a Rubber Slitter Cutting Machine
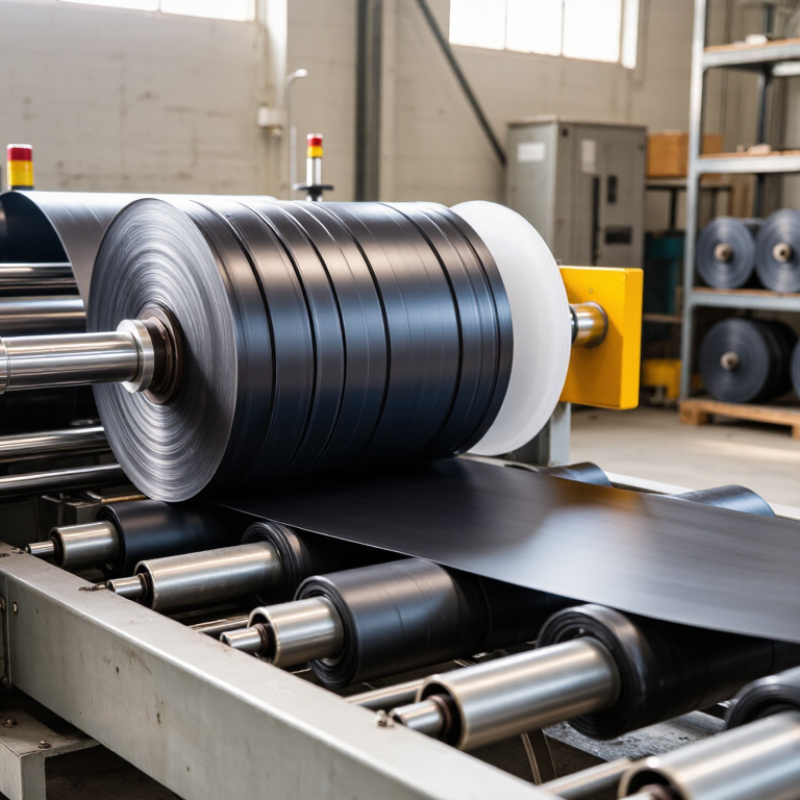
A rubber slitter cutting machine cuts wide rubber sheets or rolls into narrower strips. Operators adjust blade spacing, feed speed, and material tension to match the job. At the machine, rubber passes beneath rotating or fixed blades; the cut strips are then prepared for processes such as molding, hose production, or gasket fabrication. The machine’s industrial role is practical: it turns bulky stock into consistent widths that downstream equipment can handle. A neat cut is not the whole story.
The International Rubber Study Group’s World Rubber Industry Outlook (2024) estimated global rubber demand at about 31 million tonnes for 2024. That figure describes market demand, not slitter output, but it shows the scale of rubber processing. In production, even a small width variation can cause problems during feeding or assembly. Blade condition, sheet thickness, and rubber temperature all matter. Operators may need to adjust settings between batches; the “perfect” setup is not always obvious.
Tips: Check blade sharpness and alignment before a run. Test a short strip, then measure its width at several points. Watch for edge tearing or material drift. If the rubber warms or stretches, pause and reassess tension rather than trusting the first setting.
Main Components: Feed Rollers, Slitting Blades, and Drive System
What Is a Rubber Slitter Cutting Machine?
Main Components: Feed Rollers, Slitting Blades, and Drive System
A rubber slitter cutting machine turns a wide rubber sheet or roll into narrower strips. Its results depend on three parts working together: feed rollers, slitting blades, and the drive system. Feed rollers grip the material and guide it beneath the blades. Their pressure must be even. Too little pressure can let rubber wander; too much may flatten soft stock or leave marks. Operators can check alignment with a sample strip, because rubber may stretch and spring back after cutting.
Slitting blades create the edges. Depending on the machine and rubber type, knives may cut against an anvil or use a shearing action. Blade sharpness, spacing, and setup affect strip width and edge quality. The drive system powers the rollers and cutting components, while speed controls how steadily material passes through. A fast setting is not always better; heat and tension can distort some compounds. I still inspect the first few strips. A clean-looking setup can hide slight drift.
Tips: Start with a short test run. Measure strips after they relax, not only while under tension. Keep hands clear and follow the machine’s operating instructions.
Operating Sequence: Feeding, Blade Adjustment, Slitting, and Strip Collection
What Is a Rubber Slitter Cutting Machine?
A rubber slitter cutting machine turns wide sheets or rolls into narrower strips. The operating sequence begins with feeding: center the roll, check its edges, and guide the material evenly through the rollers. Keep the sheet flat. A small wrinkle can shift the cut. Set feed tension carefully, since soft rubber may stretch while moving.
Before slitting, adjust blade spacing to match the required strip widths. Check blade condition and alignment, then make a short test cut. Measure the strips instead of trusting the machine scale alone. During production, watch for edge tearing, heat buildup, or drifting material. Stop the feed before making manual adjustments.
The U.S. Bureau of Labor Statistics reported a 2.7 recordable injury rate per 100 full-time workers in manufacturing in its 2022 Survey of Occupational Injuries and Illnesses. That sector-wide figure is not specific to slitting, but it supports keeping guards in place and hands clear of moving blades.
At collection, separate and stack strips without pulling them taut. Inspect the edges and label each bundle. The last step sounds simple; it is easy to rush.
Material Data: Shore A Hardness (0–100), Sheet Thickness, and Feed Speed
What Is a Rubber Slitter Cutting Machine?
Material Data: Shore A Hardness (0–100), Sheet Thickness, and Feed Speed
Rubber hardness affects how a sheet responds to a slitter blade. Shore A readings use a 0–100 scale, but the number does not directly predict cutting force. ASTM D2240-15(2021) describes durometer testing, where specimen thickness, temperature, and technique can influence readings. Record the test method and conditions with each material lot. A 60 Shore A sheet may still behave differently after aging or formulation changes. Small differences matter.
Measure sheet thickness across the working width, not only at one edge. A thicker spot can lift the sheet, change blade engagement, and produce strips with uneven edges. ISO 23529:2016 outlines general procedures for preparing and conditioning rubber test pieces, supporting controlled conditions when comparing measurements. Use a calibrated gauge and note the temperature. This step is easy to miss.
Feed speed depends on hardness, thickness, blade condition, and the required edge quality. No single speed suits every rubber compound. Run a short trial, then check for tearing, heat marks, and width variation before increasing speed. Log the setting for each batch. A clean edge is useful evidence, but not proof; recheck after changing the blade.
Performance Metrics: Slit Width, Cutting Tolerance, and Output Rate
A rubber slitter cutting machine turns a continuous rubber sheet or roll into narrower strips. Its first key metric is slit width: the distance across each finished strip, not merely the blade setting. Measure samples from the beginning, middle, and end of a run. Rubber can stretch, compress, or wander under uneven tension. Small changes matter when strips must fit a downstream assembly.
Cutting tolerance describes the difference between the target width and measured widths. ASTM D3767 provides practices for measuring rubber dimensions, while ISO 3302-1 sets tolerance classes for rubber products. These references help define measurement and product expectations; they do not establish one universal slitter tolerance. Report the target, observed range, sample count, and measurement method. Be honest about variation. A neat average can hide a poor edge.
Output rate needs similar care. Record feed speed, number of lanes, and usable running time; a fast feed alone does not prove high production. For example, an eight-lane setup at 12 metres per minute produces 96 lane-metres per minute before stoppages. That is a calculated illustration, not an industry benchmark. Track scrap and changeover time too. Real runs are messier. A short trial may miss blade wear, warm-up effects, or tension drift, so verify performance over a representative production period.